Hey there! As a supplier in the by machining industry, I’ve had my fair share of experiences dealing with all sorts of materials. Today, I wanna talk about one of the more tricky ones: soft materials. Machining soft materials can be a real headache if you don’t know what you’re doing. But don’t worry, I’m gonna share some of the best practices I’ve picked up over the years. By Machining
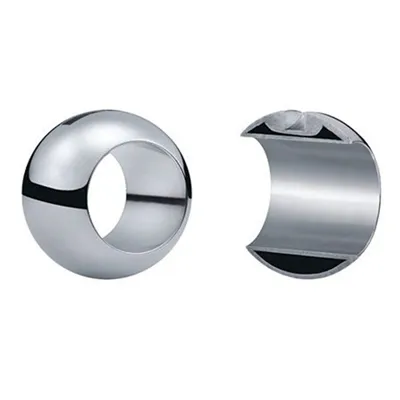
First off, let’s talk about what we mean by soft materials. Generally, these are materials that are easy to deform, like plastics, rubber, and some non – ferrous metals such as aluminum and copper. These materials have unique properties that make them different from harder materials like steel.
Tool Selection
The choice of tools is crucial when machining soft materials. For starters, you wanna go for sharp tools. Dull tools can cause all sorts of problems, like excessive heat generation, poor surface finish, and even material deformation.
When it comes to cutting tools for plastics, carbide – tipped tools are a great option. They stay sharp longer and can handle the relatively low cutting forces required for plastics. For example, if you’re machining acrylic, a carbide end mill with a high helix angle will help evacuate chips quickly and prevent the material from melting due to heat buildup.
For softer non – ferrous metals like aluminum, high – speed steel (HSS) tools also work well. HSS tools are more forgiving and can be resharpened easily. However, if you’re doing high – volume production, carbide tools might be a better long – term investment.
Cutting Parameters
Getting the right cutting parameters is just as important as tool selection. The three main cutting parameters are cutting speed, feed rate, and depth of cut.
Cutting speed is how fast the tool moves relative to the workpiece. For soft materials, you generally want to keep the cutting speed relatively high. For plastics, a cutting speed of around 800 – 1200 surface feet per minute (SFM) is usually good. Higher cutting speeds can help reduce the likelihood of the material sticking to the tool.
Feed rate is how fast the workpiece moves towards the tool. For soft materials, a higher feed rate can be used compared to harder materials. This helps prevent the tool from rubbing against the material, which can cause heat and deformation. A good rule of thumb is to start with a feed rate of around 0.002 – 0.005 inches per tooth when machining plastics.
Depth of cut is how much material is removed in each pass. When machining soft materials, a shallower depth of cut is often better. This reduces the cutting forces and helps prevent the material from deforming. For plastics, a depth of cut of 0.01 – 0.03 inches is a good starting point.
Coolant and Lubrication
Soft materials can generate a lot of heat during machining, especially if the cutting parameters are not right. That’s where coolant and lubrication come in.
For plastics, using a coolant might not always be necessary. In fact, some plastics can absorb water from the coolant, which can cause dimensional changes. However, if you’re machining at high speeds or with a large depth of cut, a light mist of a dry lubricant can help reduce friction and heat.
When machining non – ferrous metals like aluminum, a coolant is almost always necessary. A water – soluble coolant can help keep the temperature down, flush away chips, and improve the surface finish. Just make sure to use the right concentration of coolant to avoid corrosion.
Chip Management
Chips are another big issue when machining soft materials. Soft materials tend to produce long, stringy chips that can get wrapped around the tool or the workpiece. This can cause damage to the tool and the workpiece, and it can also affect the surface finish.
To manage chips effectively, you can use tools with internal coolant channels. The coolant can help break up the chips and flush them away. Another option is to use chip breakers on the cutting tools. Chip breakers are small grooves or notches on the cutting edge that help break the chips into smaller, more manageable pieces.
Workholding
Proper workholding is essential when machining soft materials. Since these materials are easy to deform, you need to make sure they are held securely without applying too much pressure.
For plastics, vacuum workholding can be a great option. It provides a uniform holding force without deforming the material. You can also use soft jaws on a vise to hold the workpiece. Soft jaws are made of a softer material than the workpiece, so they won’t damage the surface.
When machining non – ferrous metals, a conventional vise can be used, but make sure to use protective pads to prevent marring of the surface. You can also use clamps, but make sure they are evenly distributed to avoid warping the workpiece.
Quality Control
Finally, quality control is a must in machining soft materials. Since these materials are more prone to deformation and surface finish issues, you need to check the parts regularly.
You can use measuring tools like micrometers, calipers, and height gauges to check the dimensions of the parts. For surface finish, a surface roughness tester can be used. If you find any issues, you can adjust the cutting parameters or the tool as needed.
In conclusion, machining soft materials has its challenges, but if you follow these best practices, you can achieve great results. Whether you’re working on a small – scale project or in high – volume production, these tips can help you improve your efficiency and the quality of your parts.
If you’re in need of machining services for soft materials, don’t hesitate to reach out. We’ve got the experience and the expertise to handle all your by machining needs. Drop us a line and let’s start a conversation about your project.
By Port References
- "Metal Cutting Principles" by J. A. Kozak
- "Machining of Plastics" by The Society of the Plastics Industry, Inc.
- "Manufacturing Engineering and Technology" by S. Kalpakjian and S. R. Schmid
Zhejiang Jigong Valve Co., Ltd.
Address: Dongou Industrial Park, Oubei Subdistrict, Yongjia County, Wenzhou City, Zhejiang Province (within Zhejiang Yinhe Machinery Manufacturing Co., Ltd.)
E-mail: Sales@cnzjsk.com.cn
WebSite: https://www.ball-china.com/
